Introduction to Industrial By – product Gas Recovery Unit
Industrial by – product gas recovery units are essential equipment in modern industrial processes. These units are designed to capture, purify, and reuse the by – product gases generated during various industrial operations such as steelmaking, chemical production, and power generation. By recovering these gases, industries can not only reduce their environmental impact by minimizing emissions but also achieve significant economic benefits by reusing the recovered gases as energy sources or raw materials. This not only conserves natural resources but also helps in meeting strict environmental regulations. Industrial By-product Gas Recovery Unit
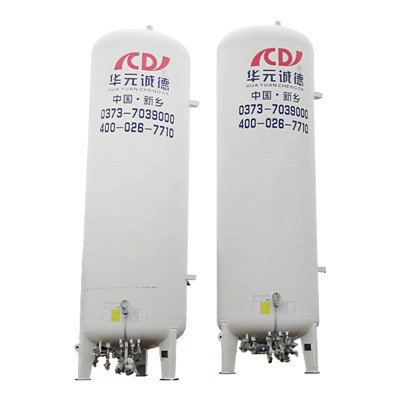
Top 10 Manufacturers
1. Xinxiang Jiale Intelligent Equipment Co., Ltd.
Xinxiang Jiale Intelligent Equipment Co., Ltd. is a leading enterprise specialized in the research, development, production, and sales of industrial equipment. With state – of – the – art R & D facilities and a highly skilled technical team, the company is committed to providing high – quality and innovative industrial by – product gas recovery units. The company adheres to strict quality control standards throughout the production process, from raw material selection to the final product assembly.
Features in Industrial By – product Gas Recovery Unit:
- High – efficiency recovery: Their units are designed to achieve high recovery rates of by – product gases, minimizing waste and maximizing resource utilization.
- Advanced purification technology: Utilize advanced purification processes to ensure the recovered gases meet high – quality standards for reuse.
- Customized solutions: Capable of providing tailored solutions according to the specific requirements and production processes of different industries.
Advantages: - Strong R & D capabilities: Continuously invest in research and development to introduce new and improved products.
- Good after – sales service: Provide comprehensive after – sales support, including installation, maintenance, and technical training.
- Cost – effective products: Offer competitive prices without compromising on product quality.
Website: https://www.jialeasu.com/
2. Linde Plc
Linde is a global leader in industrial gases and engineering. With a long – standing history and a vast global presence, it has extensive experience in gas separation and purification technologies. Linde’s engineering division specializes in designing and building large – scale industrial by – product gas recovery units for a wide range of industries.
Features in Industrial By – product Gas Recovery Unit:
- Cutting – edge technology: Incorporate the latest gas separation and purification technologies, such as cryogenic distillation and pressure – swing adsorption.
- Large – scale projects: Have the ability to handle large – scale industrial projects, providing complete turn – key solutions.
- Reliable operation: Their units are known for their reliable and stable operation, ensuring continuous gas recovery.
Advantages: - Global network: Can provide support and services worldwide, with local teams available for on – site assistance.
- Technical innovation: Constantly push the boundaries of technology to improve the performance of their gas recovery units.
- Industry reputation: Enjoy a high reputation in the industry for its quality products and services.
3. Air Liquide
Air Liquide is a major player in the industrial gas sector. It offers a comprehensive range of services and products related to gas production and management. In the field of industrial by – product gas recovery, Air Liquide has developed advanced technologies and solutions.
Features in Industrial By – product Gas Recovery Unit:
- Integrated solutions: Provide integrated solutions that include gas recovery, purification, and utilization, optimizing the overall process.
- Energy – efficient design: Focus on energy – efficient design to reduce operating costs for customers.
- Monitoring and control systems: Equip the units with advanced monitoring and control systems for real – time operation adjustment.
Advantages: - Sustainable development: Strongly committed to sustainable development, which leads to environmentally friendly gas recovery solutions.
- Technical expertise: Have a large team of experts with in – depth knowledge of gas technologies.
- Customer – centric approach: Tailor solutions according to the specific needs and goals of each customer.
4. Praxair, Inc. (now part of Linde)
Praxair was a well – known provider of industrial gases and related equipment before its merger with Linde. It had a long history of developing and manufacturing high – performance industrial by – product gas recovery units.
Features in Industrial By – product Gas Recovery Unit:
- Robust construction: The units are built with high – quality materials, ensuring long – term durability.
- Flexible configuration: Can be configured to adapt to different types of industrial processes and gas compositions.
- High – precision measurement: Incorporate high – precision measurement devices for accurate gas analysis and control.
Advantages: - Proven track record: Have a long – standing and successful track record in the industry, with many satisfied customers.
- Comprehensive service: Offer a full range of services, from equipment installation to long – term maintenance.
- Industry knowledge: Deep understanding of various industries’ gas requirements and challenges.
5. Siemens Energy
Siemens Energy is a global energy technology company. It combines advanced engineering and digital technologies to develop innovative industrial by – product gas recovery solutions.
Features in Industrial By – product Gas Recovery Unit:
- Digital integration: Integrate digital technologies, such as automation and data analytics, for intelligent operation and optimization.
- High – performance compressors: Use high – performance compressors to ensure efficient gas compression and transportation.
- Modular design: Adopt modular design for easy installation, expansion, and maintenance.
Advantages: - Digital expertise: Leverage its digital capabilities to improve the efficiency and reliability of gas recovery units.
- Global service network: Provide global after – sales service and support, ensuring quick response times.
- Research and development strength: Continuously invest in R & D to stay at the forefront of technology.
6. Mitsubishi Heavy Industries, Ltd.
Mitsubishi Heavy Industries is a diversified industrial manufacturer with a strong focus on energy and environmental technologies. It has developed advanced industrial by – product gas recovery units for various industries.
Features in Industrial By – product Gas Recovery Unit:
- Advanced heat exchange technology: Incorporate advanced heat exchange technology to improve energy efficiency during the gas recovery process.
- High – pressure resistance: The units are designed to withstand high – pressure conditions, making them suitable for many industrial applications.
- Safety features: Equip the units with comprehensive safety features to ensure safe operation.
Advantages: - Technological heritage: Benefit from a long – standing technological heritage and experience in heavy – industry manufacturing.
- Quality control: Have strict quality control systems in place to ensure the reliability of its products.
- System integration capabilities: Ability to integrate gas recovery units into complex industrial systems.
7. Honeywell International Inc.
Honeywell is a multinational conglomerate that offers a wide range of technologies and solutions. In the area of industrial by – product gas recovery, it provides advanced control and automation systems.
Features in Industrial By – product Gas Recovery Unit:
- Intelligent control systems: Develop intelligent control systems that can optimize the operation of gas recovery units in real – time.
- Alarm and monitoring functions: The systems are equipped with comprehensive alarm and monitoring functions to ensure the safety and stability of the operation.
- Remote operation and management: Allow for remote operation and management of gas recovery units, increasing operational flexibility.
Advantages: - Automation leadership: Leading position in the field of automation technology, which can enhance the efficiency of gas recovery.
- Global presence: Have a global presence, enabling it to provide support to customers around the world.
- Innovation – driven: Continuously innovate to improve the performance of its control and automation solutions.
8. Kawasaki Heavy Industries, Ltd.
Kawasaki Heavy Industries is a major industrial manufacturer with expertise in engineering and manufacturing. It has developed high – quality industrial by – product gas recovery units, especially for the steel and chemical industries.
Features in Industrial By – product Gas Recovery Unit:
- High – efficiency gas treatment: Their units are capable of effectively treating different types of by – product gases, removing impurities and recovering valuable components.
- Low – noise operation: Designed with noise – reduction features, suitable for installation in various industrial environments.
- Long – term stability: Provide long – term stable operation, minimizing downtime and maintenance requirements.
Advantages: - Engineering strength: Strong engineering capabilities to design and manufacture complex gas recovery installations.
- Product reliability: A reputation for producing reliable and durable industrial equipment.
- Application experience: Rich experience in applying gas recovery units in specific industries.
9. Air Products and Chemicals, Inc.

Air Products and Chemicals is a leading industrial gas company. It offers a variety of gas separation and recovery technologies for different industrial by – product gases.
Features in Industrial By – product Gas Recovery Unit:
- Specialized gas separation: Develop specialized gas separation processes for different types of industrial by – product gases.
- Process optimization: Continuously optimize the gas recovery process to improve efficiency and reduce costs.
- Compact design: Some of their units have a compact design, suitable for limited – space installations.
Advantages: - Gas expertise: In – depth knowledge of different gases and their properties, enabling effective gas recovery.
- Customer support: Provide comprehensive customer support, from project planning to on – site operation.
- Industry partnerships: Have established partnerships with many industries, which helps in developing customized solutions.
10. Atlas Copco AB
Large Scale Air Separation Unit Atlas Copco is a global industrial company known for its compressors, vacuum solutions, and other industrial equipment. In the context of industrial by – product gas recovery, it offers high – performance compressors and related equipment.
Features in Industrial By – product Gas Recovery Unit:
- Energy – saving compressors: Their compressors are designed with energy – saving features, reducing the overall energy consumption of the gas recovery system.
- High – reliability compressors: Known for the high – reliability of its compressors, ensuring continuous gas recovery.
- System integration with compressors: Can integrate compressors seamlessly into the entire gas recovery unit system.
Advantages: - Compressor technology leadership: Leading in compressor technology, which is crucial for the gas recovery process.
- Global service network: Provide global after – sales service and support, ensuring quick availability of spare parts and technical assistance.
- Product innovation: Continuously innovate to introduce more efficient and reliable compressor products.
